Ammonia compressors
Refrigeration and process duty on a gas that attacks the wrong materials.
Technical data
- Free air delivery
- 100 – 3,500 Nm³/h
- Working pressure
- 16 – 40 bar g
- Motor power
- 6 – 75 kW
Overview
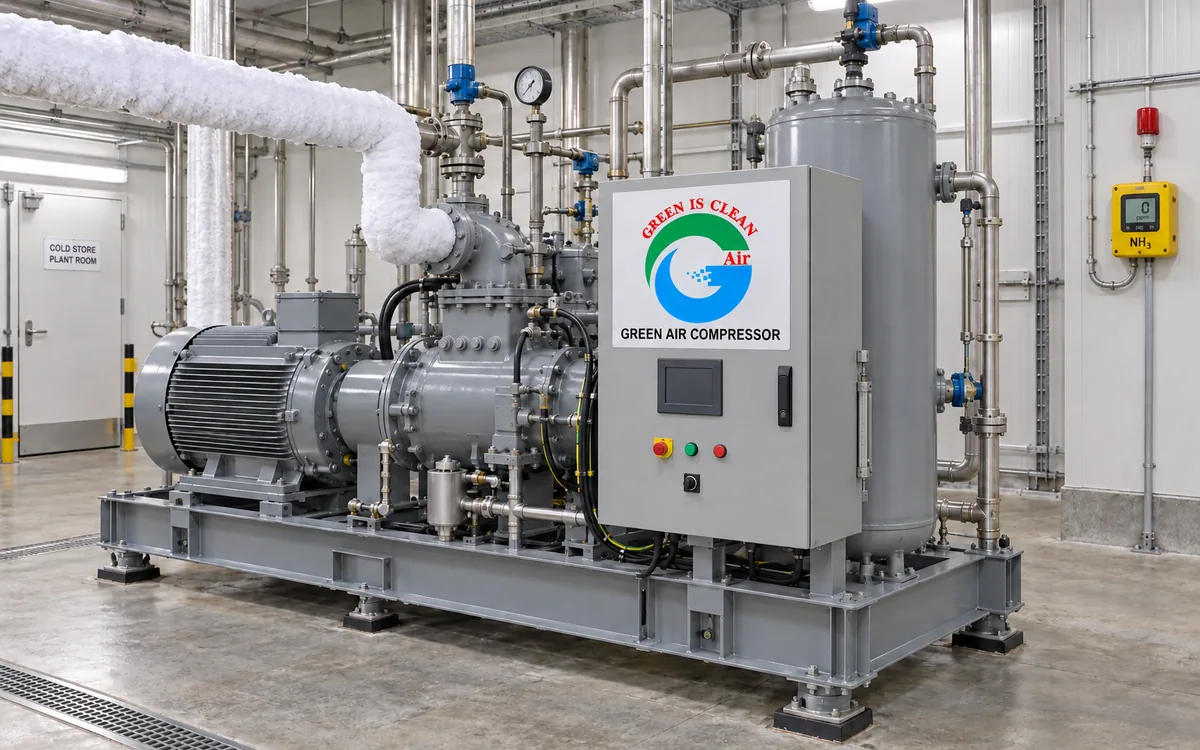
Ammonia is an excellent refrigerant — high latent heat, cheap, and with no ozone or global warming penalty — which is why industrial cold stores and food plants keep using it. It is also toxic and it attacks copper and copper alloys, so the machine and everything around it is built in steel.
These are compressors for industrial refrigeration and for process ammonia duties, built with no copper in the gas path, with seals selected for ammonia, and with the safety instrumentation the gas requires.
Key benefits
No copper in the gas path
Ammonia attacks copper and its alloys. Wetted parts are steel and the seals are chosen to suit.
Built for refrigeration duty
Economiser ports, oil management and capacity control arranged for a refrigeration circuit rather than for air.
Safety instrumentation included
Detection, isolation and the shutdown logic the gas demands, specified with the machine.
Screw and reciprocating
Screw for continuous plant duty, reciprocating where the load is small or highly variable.
Why plants keep choosing ammonia
Thermodynamically it is very hard to beat. An ammonia plant uses meaningfully less energy than the equivalent on a synthetic refrigerant, and the refrigerant itself costs almost nothing to replace.
It also has no phase out date. Synthetic refrigerants have been through several generations of regulation and each one has stranded somebody's plant. Ammonia has been used for over a century and no regulator is proposing to ban it.
The cost is that it is toxic and it must be engineered properly: machinery room ventilation, detection, and an emergency plan. That is a design cost rather than a running cost, and for a plant of any size it is repaid quickly.
- Lower energy than synthetic refrigerants
- No phase out risk
- Cheap to replace
- Steel gas path, no copper
- Machinery room ventilation and detection required
- Economised screw or reciprocating builds
What we need to quote
Gas compressors are not selected from a catalogue. The gas itself decides the materials, the seals and the safety case, and two plants asking for the same machine on paper often need different builds.
Four answers cover most of it: the gas and its composition, the suction pressure and temperature, the discharge pressure required, and the flow. With those we can size the machine and tell you whether it should be a screw, a reciprocating or a centrifugal.
Then the site questions. Area classification, whether the gas is wet or contains hydrogen sulphide, what the local authority requires, and whether the duty can stop. Those decide the seal arrangement and whether you need one machine or two.
- Gas composition and molecular weight
- Suction pressure and temperature
- Discharge pressure required
- Flow, normal and maximum
- Area classification
- Whether the duty can be interrupted
Model range
- 25 bar g
- 100 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 40 bar g
- 260 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 30 bar g
- 300 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 25 bar g
- 220 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 30 bar g
- 420 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 40 bar g
- 510 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 30 bar g
- 540 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 40 bar g
- 660 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 25 bar g
- 330 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 24 bar g
- 550 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 30 bar g
- 630 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 16 bar g
- 450 Nm³/h
- Dimensions L x W x H
- 1100 × 740 × 960 mm
- 24 bar g
- 750 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 24 bar g
- 920 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 16 bar g
- 600 Nm³/h
- Dimensions L x W x H
- 1100 × 740 × 960 mm
- 16 bar g
- 750 Nm³/h
- Dimensions L x W x H
- 1100 × 740 × 960 mm
- 24 bar g
- 1,380 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 16 bar g
- 950 Nm³/h
- Dimensions L x W x H
- 1400 × 900 × 1180 mm
- 30 bar g
- 1,710 Nm³/h
- Dimensions L x W x H
- 1400 × 900 × 1180 mm
- 16 bar g
- 1,200 Nm³/h
- Dimensions L x W x H
- 1400 × 900 × 1180 mm
- 24 bar g
- 1,500 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 16 bar g
- 1,500 Nm³/h
- Dimensions L x W x H
- 1400 × 900 × 1180 mm
- 24 bar g
- 1,880 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 16 bar g
- 1,800 Nm³/h
- Dimensions L x W x H
- 1400 × 900 × 1180 mm
- 24 bar g
- 2,250 Nm³/h
- Dimensions L x W x H
- 1000 × 580 × 870 mm
- 24 bar g
- 3,000 Nm³/h
- Dimensions L x W x H
- 1600 × 900 × 1200 mm
- 24 bar g
- 3,500 Nm³/h
- Dimensions L x W x H
- 1600 × 900 × 1200 mm
FAD measured to ISO 1217 Edition 4, Annex C and E at 1 bar a intake, 20°C, 0% humidity. Noise measured to ISO 2151 in free field conditions, tolerance ± 3 dB(A). Water-cooled versions of every model are available. Ask us for their sheet.
Frequently asked questions
Is ammonia safe to use?
It is used safely at scale across the world, and the engineering that makes it safe — ventilation, detection, isolation — is well established. It is not a system to improvise.
Why not a synthetic refrigerant?
Higher energy cost, expensive refrigerant, and a regulatory history of phase outs. For an industrial plant of any size ammonia usually wins on both counts.
Can existing copper pipework be used?
No. Ammonia attacks copper and its alloys. The circuit has to be steel throughout, including anything reused from an earlier plant.
How much less energy does it use?
Typically ten to twenty per cent against a synthetic refrigerant plant of the same duty, and the refrigerant itself costs almost nothing to replace.
What does the machinery room need?
Ventilation, gas detection, emergency isolation and an emergency plan. It is a design cost rather than a running cost and it is not optional.
Screw or reciprocating?
Screw for continuous plant duty and economised operation; reciprocating where the load is small or highly variable. We size both and show the comparison.
What is an economiser port?
A second suction at an intermediate pressure. It increases capacity and efficiency on a refrigeration cycle and is one of the reasons screw machines dominate this duty.
How is the oil managed?
Separated, cooled and returned, with the level monitored. Oil carried into the evaporator is the commonest cause of lost capacity on an ammonia plant.
Can you service it locally?
Yes, and parts are held rather than shipped on demand. An ammonia plant that stops is a cold store warming up, so response time matters more than usual.
Does the plant need certification?
Yes, and the requirements differ across the countries we trade in. We state which apply and supply the documentation to match before the order.
Related products
Nitrogen compressors
Boosting and circulating nitrogen for blanketing, purging and process.
- Free air delivery
- 90 – 3,000 Nm³/h
- Working pressure
- 3 – 160 bar g
- Motor power
- 22 – 250 kW
Oxygen compressors
Oil free by necessity, built and cleaned to oxygen service standards.
- Free air delivery
- 30 – 120 Nm³/h
- Working pressure
- 120 – 150 bar g
- Motor power
- 11 – 30 kW
Biogas compressors
Wet, corrosive, variable gas handled without eating the machine.
- Free air delivery
- 50 – 700 Nm³/h
- Working pressure
- 5 – 45 bar g
LPG and hydrocarbon gas compressors
Transfer, recovery and vapour handling for propane, butane and mixed gas.
- Working pressure
- 16 bar g
- Motor power
- 4 – 110 kW
Not sure which model you need?
Send us your air demand, working pressure and running hours. Our engineers will size the machine and send a written recommendation, no cost, no obligation.