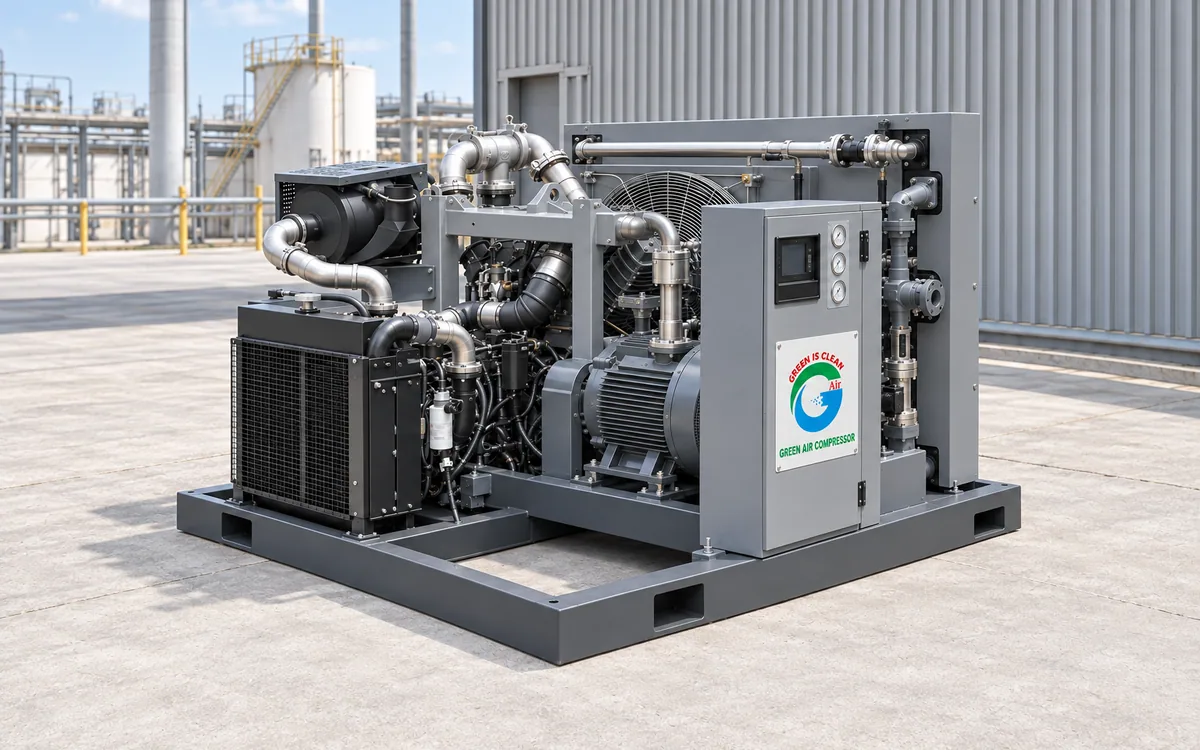
High pressure booster compressors
Portable boosters taking site air up to 40 bar.
Technical data
- Free air delivery
- 10.0 – 16.0 m³/min
- Working pressure
- 7 – 40 bar g
- Motor power
- 75 – 129 kW
Overview
Some site jobs need far more pressure than a standard portable compressor delivers: deep hole drilling, pipeline testing, or driving down-the-hole hammers at depth.
A portable booster takes the 7 to 10 bar output of the compressor you already have on site and raises it to 25 or 40 bar, which is much cheaper and more practical than mobilising a dedicated high pressure machine.
Key benefits
Works with the machine you have
Boosts existing site air rather than requiring a second large compressor.
25 or 40 bar output
Covers deep drilling and pipeline pressure testing duties.
Trailer or skid mounted
Moves with the rest of the site fleet.
Diesel driven
Independent of site power, matched to the compressor it works with.
How it is built
A booster raises air that has already been compressed, so it reaches high pressure from a site compressor without a separate high pressure machine on the job.
On construction work that matters because the alternative is transporting and fuelling a second compressor for one part of the task, usually pipeline testing or drilling.
The cylinders, valves and cooling are specified for the discharge temperature that a second stage creates, and the intercoolers are what keeps that temperature survivable.
- Raises site compressor air to high pressure
- No second compressor needed on site
- Intercooling between stages
- Skid or trailer mounted
- Suits pipeline testing and drilling
- Diesel or electric drive
- Relief and isolation to the applicable standard
- Hire or purchase
On site controls
Inlet and discharge pressure are both watched. A booster starved of inlet air runs hot and damages itself long before anything downstream shows a problem.
The panel shows discharge temperature as well as pressure, because on a booster the temperature is the reading that predicts a valve problem weeks ahead.
It stops on the receiver rather than cycling against a valve, which is what keeps valve and ring life where the intervals assume it will be.
- Inlet and discharge pressure monitored
- Low inlet pressure protection
- Discharge temperature shown and alarmed
- Receiver control rather than valve cycling
- Running hours and service countdown
- Fault history kept on the machine
- Fleet telemetry available
- Automatic restart after a power failure
Parts and service
Valves and rings on published intervals, plus the engine service on diesel driven units.
A booster that has lost valve condition still delivers air, just less of it and at more fuel. Flow at pressure is therefore recorded at every service so the decline is visible.
We service these on site with the rest of the fleet, because moving a skid for a service costs more than the service.
- Valve kits at the published interval
- Ring and seal kits by interval
- Engine service on diesel units
- Flow at pressure recorded at every service
- Serviced on site with the fleet
- Held in local stock
- Hire fleet servicing available
- Fixed price under a service plan
Model range
- 7 → 25 bar
- 10.0 m³/min
- 7 → 40 bar
- 16.0 m³/min
Performance to ISO 1217 Annex C at 20 °C inlet, 1 bar(a). Figures are typical and subject to confirmation. Ask us for the certified test report for your selected model.
Frequently asked questions
What pressures are we talking about?
Typically 40 to 350 bar and beyond, depending on the duty. Above that you are into specialist breathing air and industrial gas territory.
What is it used for?
Cylinder filling, pressure and burst testing, seat testing on valves, gas injection, and PET blowing at the higher end.
Can it feed breathing air?
Only with a dedicated breathing air purification package and monitoring. Never take breathing air from an industrial booster without it. This is a life safety matter.
How is the pressure controlled?
By pressure switches and relief valves at each stage, plus a final regulator. Every stage needs its own protection, not just the outlet.
What safety equipment is required?
Relief valves per stage, burst discs where specified, rated hose and fittings, and a documented inspection regime for the vessels.
Does high pressure need special pipework?
Yes: rated tube and fittings, correctly supported, with no improvised joints. High-pressure gas failures are dangerous in a way low-pressure air is not.
How much does moisture matter?
Enormously. Water at 300 bar behaves very differently, and a high-pressure dryer is normally essential rather than an option.
What is the maintenance interval?
Shorter than on general compressors, valve and seal service at set hours. We build the schedule into the quotation so it is not a surprise later.
Can you supply the vessel certification?
Yes, with the machine, and we handle the periodic re-inspection as part of the service contract.
Is training included?
Yes, and we require it. High-pressure equipment operated by an untrained person is the single biggest risk in this product range.
Not sure which model you need?
Send us your air demand, working pressure and running hours. Our engineers will size the machine and send a written recommendation, no cost, no obligation.